CIGS Three-Curve Solar Tile Peeling: The ETFE Delamination Failure Explained
Oct 14, 2026
L
Luke
Product Manager, GreenMore · Photovoltaic building materials
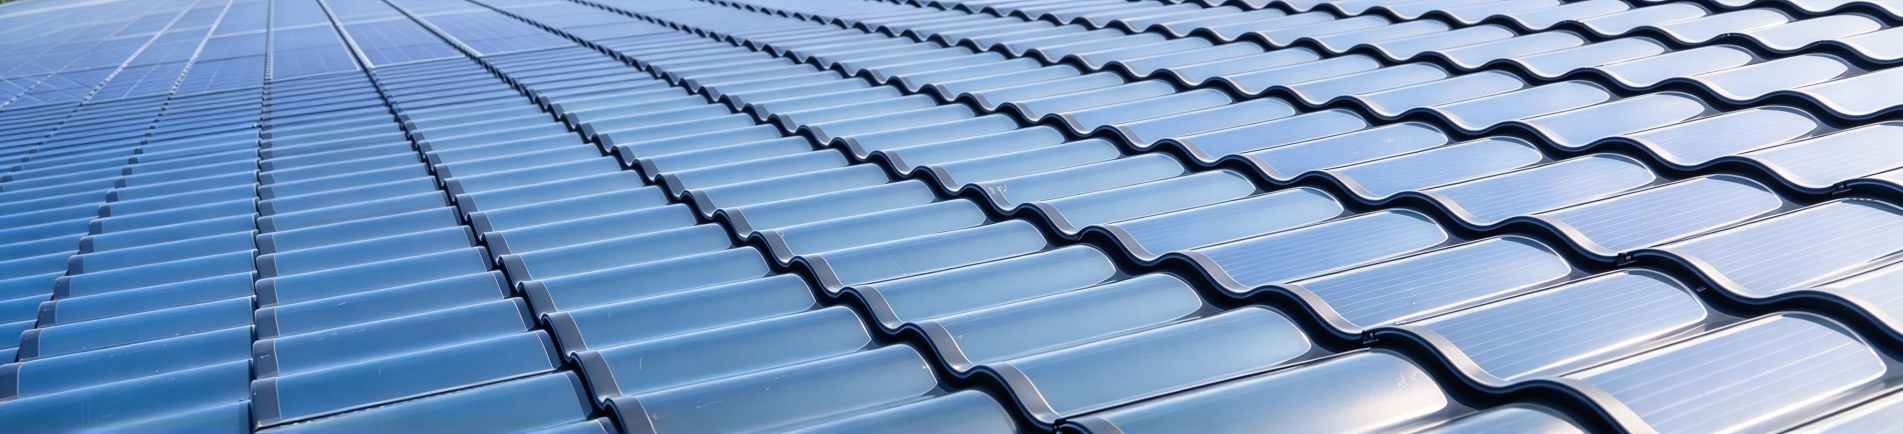
Thin-film three-curve solar tiles are one of the most architecturally integrated BIPV options on the market. Their curved CIGS (copper indium gallium selenide) layer, ETFE front film and laminated edge sealing let them replace conventional roof tiles while generating electricity. That multi-layer build is exactly what makes them attractive — and what introduces a specific failure mode that project teams should understand: ETFE surface delamination, commonly described on site as "peeling" or "lifting."
This article explains what that failure looks like, how the multi-layer structure works, the root causes across manufacturing, installation and climate, the real risks it creates, and the checks that catch it before it becomes a roof problem.
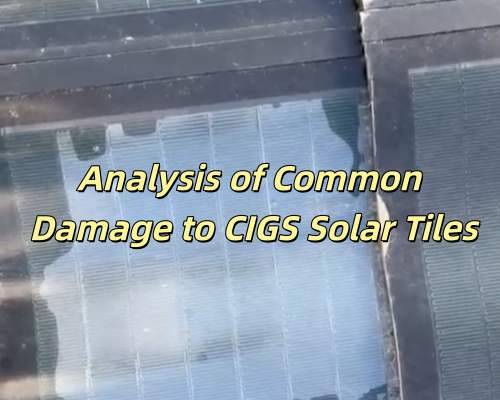
Fig 1 — ETFE surface delamination (peeling) on a curved CIGS solar tile. Replace with site photo.
What a CIGS Three-Curve Tile Is (and Why It Has Layers)
A curved solar tile is not a flat panel bent into shape. It is a laminated composite built from the outside in:
ETFE front film — a transparent, chemically inert fluoropolymer that protects the cells from UV, moisture and abrasion while transmitting light to the active layer.
Encapsulant layer — typically EVA, PVB or a specialty adhesive that bonds the ETFE to the active cell layer.
CIGS thin-film cell — the semiconductor that actually generates electricity.
Back substrate — the structural base that gives the curved tile its shape and mechanical strength.
The curved profile adds a permanent bending stress that flat panels do not carry. ETFE is chemically inert by nature, which is a good thing for durability, but it also means the surface must be specially treated (corona, plasma or primer) before the encapsulant will bond to it reliably. If that surface treatment is inconsistent, the interface between ETFE and encapsulant becomes the weakest link in the stack.
A simple way to picture the failure: imagine a multi-layer sticker on a curved surface. If the adhesive at the edge starts to lift, moisture and air get under the layers, and the lifting spreads. In a solar tile, that "lifting" is delamination.
How to Recognize Delamination on Site
Delamination has a recognizable appearance that differs from common surface defects. The main visual signs are:
Irregular whitish or opaque patches on the tile surface where the ETFE film has separated from the encapsulant beneath.
Visible bubbles or blisters under the ETFE film, often starting at edges and growing inward.
Edge seal failure — cracking, peeling or lifting of the side sealing material, sometimes with moisture visible under the seal.
Progressive spread — small affected areas that grow over weeks or months, especially after rain events.
These signs are distinct from other common issues:
Issue
How it differs from delamination
Surface dirt or bird droppings
Washes off; does not affect film adhesion
Scratches or abrasion
Linear marks on the ETFE surface, no separation
Hail damage
Localized puncture or crack, usually with a clear impact point
Hot-spot yellowing
Discoloration of the cell layer, no film lifting
Visual inspection is the first step. Where delamination is suspected, two lab tests give a clearer picture:
EL (electroluminescence) imaging — reveals micro-cracks and inactive areas in the CIGS cell beneath the delaminated zone.
Insulation resistance (IR) testing — checks whether moisture ingress has compromised the electrical isolation of the cell layer.
Fig 2 — Side-by-side comparison: (1) surface dirt, (2) hail damage, (3) edge-seal cracking, (4) ETFE delamination with bubbling. Replace with field inspection photos.
The Full Failure Chain: From Intact Tile to Peeling ETFE
Delamination is rarely a single-cause event. It is a chain of conditions that, once started, tends to accelerate. The typical sequence runs like this.
Step 1 — Edge Seal Compromise (the usual starting point)
The side seal is the first barrier against moisture. If it degrades, cracks, or is mechanically damaged during installation, rain and humidity can enter the tile interior along the edge.
Once water reaches the ETFE–encapsulant interface, it begins to hydrolyze the adhesive bond. Encapsulants are designed to be moisture-resistant, not moisture-proof at a compromised edge. The bond weakens progressively rather than failing all at once.
Step 2 — Three Acceleration Factors
Once the seal is breached, three categories of factor determine how quickly and how far delamination spreads.
2.1 Manufacturing Factors
Lamination process limits on curved tiles. Flat modules are laminated in well-established cycles of vacuum, temperature and pressure. Curved tiles introduce uneven pressure distribution across the curvature. If vacuum level, temperature profile or hold time is insufficient, the encapsulant may not cross-link completely, leaving the bond weaker than specified from day one.
ETFE surface treatment variability. If the corona or plasma treatment of the ETFE is uneven across a batch, some tiles will have lower initial adhesion than others — a latent defect that only shows up after months in the field.
Edge seal material selection. Not all sealants perform equally under UV, thermal cycling and hydrolysis. A sealant chosen primarily on cost rather than on long-term weathering data can become the limiting component.
2.2 Installation Factors (the most common on-site contributor)
Uneven batten or rail installation. A curved tile forced onto a non-flat substrate carries mechanical stress in the glass and the lamination. That stress concentrates at the edges, where the seal is.
Over-tightening of fixings. Clamping force beyond the tile's design tolerance can micro-crack the edge seal or distort the curvature, both of which open pathways for moisture.
Poor overlap drainage design. If adjacent tiles do not shed water cleanly, water can pool at the joint and sit against the edge seal for extended periods — exactly the condition that accelerates hydrolysis.
Foot traffic during installation. Walking directly on tiles can cause micro-damage to the ETFE or edge seal that is invisible at handover but becomes a failure origin months later.
2.3 Climate and Environment
Thermal cycling. Day–night and seasonal temperature swings cause the different materials in the tile (glass, ETFE, encapsulant, CIGS, substrate) to expand and contract at different rates. Each cycle slightly strains the bonded interfaces. Over thousands of cycles, fatigue accumulates.
UV exposure. Long-term UV gradually reduces the flexibility and adhesion of some encapsulants. This is a slow process (years, not months), but it lowers the threshold at which other factors trigger failure.
High humidity and freeze–thaw. In humid climates, moisture ingress is faster. In cold climates with freeze–thaw cycles, water that has entered a small defect can freeze, expand, and mechanically widen the defect.
Step 3 — Single-Event Triggers (less common but possible)
A single impact event — hail, a falling branch, dropped tools during maintenance — can create a small breach in the ETFE or edge seal. If the breach is not detected and sealed, it becomes a new entry point for moisture, and the delamination process begins from that point.
Fig 3 — Annotated cross-section of a curved CIGS tile showing moisture ingress path from a compromised edge seal through the ETFE–encapsulant interface. Replace with technical diagram.
What Happens After Delamination Starts
The consequences are not cosmetic. Once the ETFE begins to separate from the underlying layers, three things happen in parallel.
Power Output Declines
The delaminated zone no longer transmits light cleanly to the CIGS cell. Output from that area drops. If moisture reaches the cell layer itself, it can corrode the thin-film electrodes, causing a progressive and irreversible power loss that extends beyond the visibly affected area.
Electrical Safety Risks Increase
Moisture inside the tile reduces insulation resistance. In a string of tiles at system voltage, reduced insulation can lead to leakage current to ground or, in the worst case, DC arcing at a damaged interconnect. Both conditions are safety issues, not just performance issues.
Roof Waterproofing Is Compromised
The tile is simultaneously a power generator and a roof covering. A failing edge seal means the tile is also failing as a waterproofing element. Water that enters through a delaminated edge can migrate into the roof structure, with consequences for insulation, battens and the building interior.
The Practical Conclusion
A delaminated tile cannot be reliably repaired on the roof. The multi-layer bond cannot be restored in situ. The correct response is replacement of the affected tile(s) and investigation of why the failure started, so the same issue does not recur across the installation.
How to Prevent Delamination on BIPV Projects
Prevention is a combination of product selection, design, installation discipline and ongoing inspection.
Product Selection
Ask the manufacturer about the lamination process for curved tiles specifically, not just flat modules. Curvature changes the pressure profile.
Request data on ETFE surface treatment consistency across production batches.
Confirm the edge seal material specification and whether it has been tested for hydrolysis resistance, UV aging and thermal cycling — not just initial adhesion.
Where available, review accelerated aging test results (damp heat, thermal cycling, humidity-freeze) for the specific tile model.
Design and Detailing
Ensure the support structure is flat within the tile manufacturer's tolerance. A curved tile on a non-flat substrate carries built-in stress.
Specify overlap and drainage details that prevent water from pooling at tile joints.
Design fixing points and clamping forces within the tile's rated limits — not based on generic framing practice.
Installation Practice
No walking on installed tiles. Use crawl boards or roof ladders where access is needed.
Control fixing torque to the manufacturer's specification. Over-tightening is a common and avoidable cause of edge damage.
Protect edge seals during handling and stacking. Once an edge is nicked or compressed, the tile's moisture barrier is already compromised before it reaches the roof.
Operations and Maintenance
Visual inspection of edge seals at least annually, and after any severe weather event.
Periodic EL and insulation testing on a sample of tiles, especially in the first two years when latent manufacturing defects are most likely to surface.
Keep installation records including batch numbers and tile positions, so that if a failure pattern emerges, it can be traced to a specific production run or installation team.
Fig 4 — Installer inspecting edge seals on a completed curved solar tile roof. Replace with project site photo.
A Practical Field Checklist for Project Teams
When delamination is reported or suspected on a project, the following steps help separate a single-event damage case from a systemic issue.
Map the extent. Is it one tile, a cluster on one roof plane, or spread across multiple orientations? A single tile suggests impact damage. A cluster on one plane suggests a local installation issue (drainage, substrate flatness). Spread across orientations suggests a product or sealant issue.
Check overlaps and fixings in the affected area. Look for ponding water, distorted tiles, or over-tightened clamps.
Record batch numbers and installation dates for the affected tiles. Cross-reference with other projects using the same batch.
Send representative samples for lab testing — EL imaging, insulation resistance, and damp-heat aging — to confirm whether the failure is adhesion-related or moisture-corrosion related.
Decide on replacement scope. Replace affected tiles and any tiles in the same batch that show early signs. Address the root cause (design, installation, or product) before re-installation.
Summary
ETFE delamination on a curved CIGS solar tile is a multi-layer adhesion failure. It typically starts with a compromised edge seal that allows moisture to reach the ETFE–encapsulant interface. Thermal cycling, UV aging, and installation stress accelerate the process. The result is declining power output, reduced electrical insulation, and compromised roof waterproofing.
BIPV is not just a solar product — it is a building component. The tile must perform as a roof covering and as a power generator for decades. That means the materials, the manufacturing process, the roof design, and the installation all have to be right. There is no single point of failure that explains every case, and there is no single fix that covers every symptom.
GreenMore has worked on BIPV thin-film tile projects across Europe, the Middle East and Asia, including the curved triple-arch hantile range. Our role as the tile manufacturer is to support project teams from the early feasibility stage — reviewing roof design, confirming product suitability, and providing technical guidance through installation and commissioning — rather than only supplying a product and walking away. For partners planning a curved solar tile roof, we can review the roof layout, confirm the tile model and configuration, and provide a project-specific proposal. Reach us through our contact page or at export@gmsolarkit.com.
Frequently Asked Questions
Can a delaminated solar tile still generate electricity?
Partially, yes. The undamaged areas of the tile will continue to produce power. But the delaminated zone no longer contributes, and moisture ingress can progressively corrode the cell layer. A delaminated tile should be replaced rather than left in service, both for performance and for electrical safety.
Can delamination be repaired on the roof?
No. The multi-layer bond cannot be restored in situ. Attempting to re-seal or re-laminate a delaminated tile on the roof does not restore the original adhesion or insulation properties. The correct action is tile replacement.
Which climates need the most attention to edge-seal reliability?
High-humidity coastal regions, areas with large day–night temperature swings (desert climates), and regions with freeze–thaw cycles all accelerate the conditions that lead to delamination. Projects in these climates should place extra emphasis on edge-seal material selection, overlap drainage design, and post-installation inspection.
Related Reading
Three-Curve Solar Tiles: Types, Technology, and Best Roof Applications — the full comparison between CIGS thin-film and back-contact three-curve tiles.
GreenMore Israel Home Solar Roof Project — a residential project using curved solar tiles with home battery storage.
Solar Tiles Category — the full range of GreenMore solar tiles.
Customised Services (OEM/ODM) — how GreenMore supports project-specific tile and system configuration.
Updated October 14, 2026
External references: IEC 61215 (crystalline and thin-film module qualification), IEC 61730 (PV module safety qualification), EN 14782 (self-supporting metal sheet for roofing).


 Network Supported