When a BIPV Project Fails: Spares, Timelines, Repair Costs
Jul 16, 2026
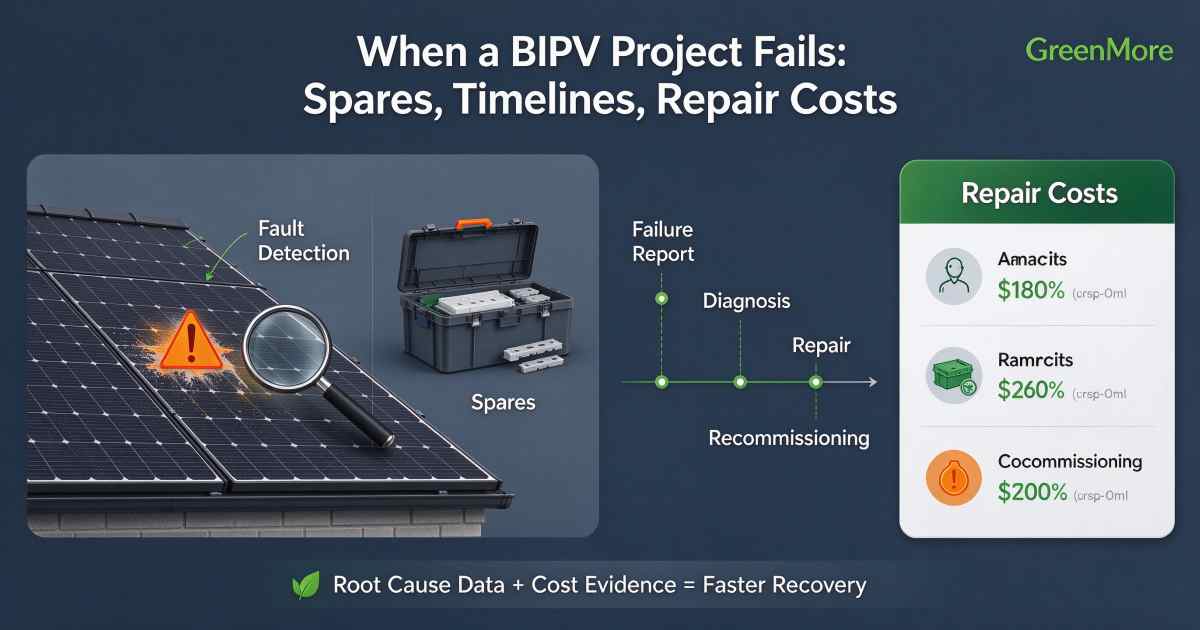
Every supplier publishes what its support covers. Very few publish what happens when something actually fails: who answers, how long it takes, what the part costs, and who pays for the flight.
That is what this page is about. It is not a list of services. The service and support page covers what GreenMore offers across planning, installation, commissioning and operation, including the training programme, documentation set and warranty terms. This page takes one narrow subject: the failure path, from the first message to the part arriving on site, with the timelines and costs attached to each step.
If you are evaluating whether the support package is adequate, read the service page. If you are planning a project and want to know what a bad week looks like and what it will cost, read this.
Most cases are resolved with three things on the table: the drawing, the log and a photograph.
How a factory-based support model behaves
GreenMore is a factory, not a service network. There are no regional service partners and no local stock of every part in every market. What exists is an engineering team at the plant that has built and commissioned these systems, reachable by email, messaging and video call, with a typical response time of 24 hours on business days.
Four consequences follow, and they are better understood before a project starts than after:
Response time is about a day, not an hour. A fault raised on Friday evening is answered on the next business day. For a residential system that is fine. For a commercial system losing revenue per hour, it argues for holding spares on site.
English is the working language. For other languages we work through a translator or machine translation. That is adequate for documents and written questions and slow for a live fault-finding call.
The first reply usually comes from your sales contact. Not because engineers are hidden, but because not every engineer is confident speaking English, and a routed question gets an accurate answer faster than a direct one that gets misread.
There is no local technician to send. Remote diagnosis is the default. An engineer attends site only when remote work has been exhausted, and the travel is charged at cost.
None of this is unusual for a manufacturing exporter. It is unusual to see it written down.
The five failures behind most support tickets
Across the projects we support, the same handful of problems keeps appearing. They are worth knowing because four of the five are installation errors rather than product faults, and all five are cheaper to prevent than to fix.
1. Communication that works but does not report
The system generates, the inverter display looks normal, and the monitoring platform shows nothing. The usual causes are RS485 or CAN wiring reversed, termination resistors missing at the end of a long bus, or a meter address set to the wrong channel.
This is the most common ticket we receive, and it is almost always resolved remotely in one session. It is also the one that damages trust most, because the owner concludes the system is broken when it is only unobserved.
2. Firmware mismatch between inverter, battery and EMS
Everything energizes, then the battery refuses to charge above a set rate because two devices disagree about the protocol version. Nothing is faulty. The fix is a version alignment, which takes minutes once identified and can take two weeks to identify if nobody thought to check the firmware builds against each other.
3. The CT clamp that charges when it should export
Fitted backwards, or clamped to the wrong conductor. The system behaves correctly according to what it measures and incorrectly according to what the building needs. On a sunny commissioning day this is invisible. On the first evening it is obvious, and by then the installer has left. The same clamp logic applies to the residential storage systems, where import and export direction decides whether the battery charges or discharges.
4. String voltage that is fine in summer
A string designed at 25 degrees can exceed the inverter window at minus 10. The commissioning reading looks acceptable, the system runs all summer, and the first cold snap takes the inverter out. This one is not an installation error at all: it is a design error that no amount of site work will correct.
The check is simple and worth doing on every project. Take the module open-circuit voltage at STC, apply the temperature coefficient at the lowest expected ambient for the site, multiply by the number of modules in the string, and compare against the inverter maximum. If it is close, shorten the string.
5. The roof detail that leaks at the valley
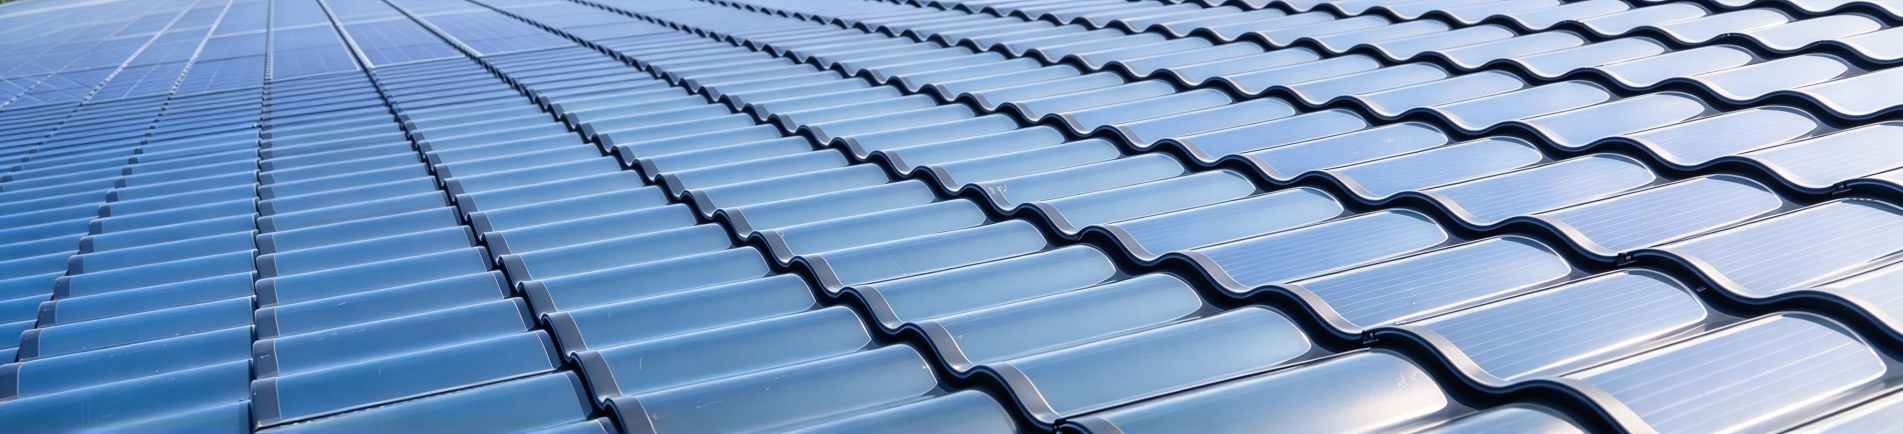
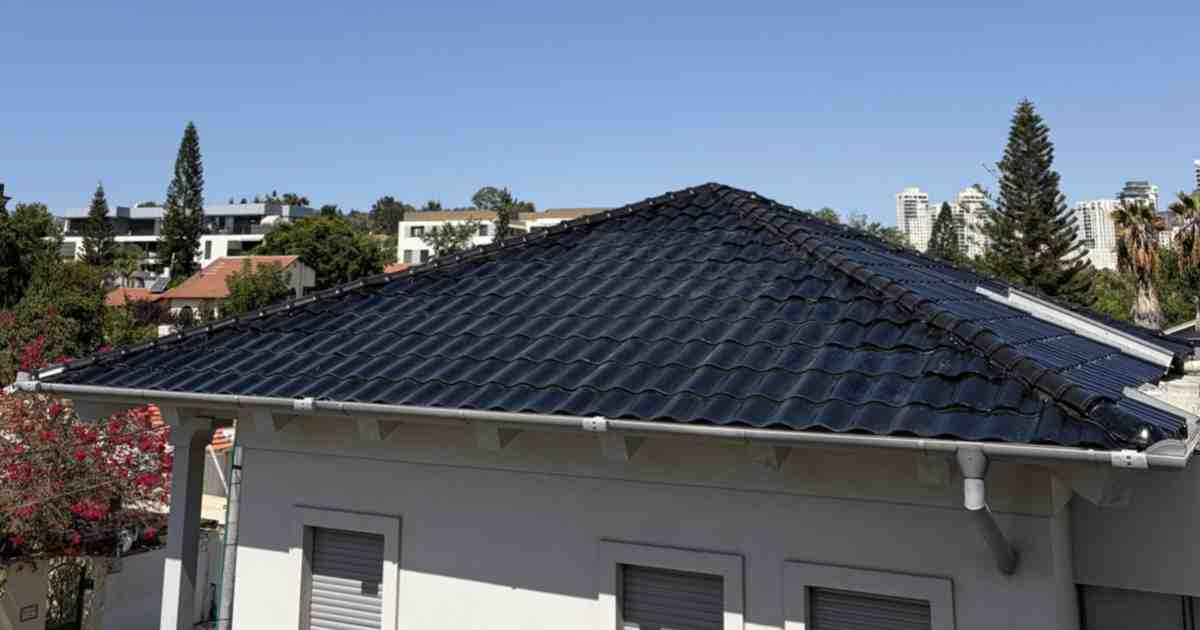
Cut tiles at a hip or valley are unavoidable. What matters is whether the cut lands on a lap or on an exposed face. A cut through the drainage channel will track water sideways, and the leak appears a metre away from where it was made. The BC curved tile carries its channel along the vertical lap for exactly this reason, which is why the cutting sequence matters more than the cutting tool. This is the only one of the five that genuinely requires a site visit in most cases, because it cannot be seen remotely.
Four of the five common failures can be diagnosed from a photograph and a log. The fifth cannot.
What a usable support request contains
The single biggest cause of delay is a request that cannot be actioned. Not a difficult fault, not a slow engineer: a message without a serial number. Without it we cannot tell which firmware build, which batch or which production revision the unit came from, and the first reply becomes a question instead of an answer.
A request that gets resolved in one round contains six things:
Model and serial number. Every unit, including batteries and inverters, not just the one that looks faulty.
Fault code or error text. Photographed from the display or exported from the platform, rather than paraphrased.
A log extract covering the period before the fault. The hour before an alarm usually explains it.
Photographs. The installation, the connector in question, the label plate, and the reading on the meter.
What changed. New firmware, new load, new tariff setting, grid outage. Most faults have a trigger.
Site conditions at the time. Weather, ambient temperature, snow cover, and whether the grid was stable.
With those, most cases close in one exchange. Without them, the case becomes a conversation, and a conversation across time zones costs days rather than hours.
How long each kind of case takes
These are working figures for a business-day timeline, from the moment a complete request arrives. They are not service-level commitments, and a case that turns out to be a hardware failure takes longer than one resolved by configuration.
Case type
First response
Resolution
What shortens it
Monitoring or communication fault
Within 24 hours
Same session in most cases
Log extract, platform access, photographs
Firmware or configuration issue
Within 24 hours
1–3 days
Current versions of all three devices
Suspected hardware failure
Within 24 hours
Diagnosis in 1–2 days, part lead time after
Serial number, fault history, meter readings
Roof or waterproofing issue
Within 24 hours
Site visit or installer rework
Photographs of the detail, not the roof
Spare part quotation
Within 24 hours
Dispatch depends on stock and shipping
Model, quantity, destination, order reference
Out-of-warranty repair
Within 24 hours
Assessment first, then part and travel
Fault history, photographs, site access
Two things are outside this table and should be planned separately: shipping time, which depends entirely on destination and customs, and site attendance, which depends on visas and flight availability. Neither can be compressed by working faster.
Language, and who you end up talking to
English support means English support. Most of our engineers read technical English well and speak it with varying confidence. For a drawing, a written diagnosis or a document, that is not a limitation. For a live fault-finding call with three people on a roof in the rain, it is.
In practice the route is: your sales contact receives the question, identifies whether it is installation, commissioning, configuration or hardware, and routes it to the right engineer. When the problem is genuinely difficult, the engineer joins directly and the sales contact stays on the call as translator. That is why the first reply often comes from a commercial contact rather than a technical one.
Two things make this work better. Written questions get written answers, which are accurate and can be forwarded to the installer. Live calls are scheduled rather than improvised, so a translator is available. If the installation team does not work in English, nominate one English-speaking coordinator on your side. It costs less than a call-out.
Spare parts: two models and the arithmetic
There are two ways to handle spares, and the right choice depends on how far the site is from the factory and what a day of downtime costs.
Model one: pre-purchased with the order
A percentage of the order quantity is configured as spares at the time of purchase, typically 3 to 5 percent depending on project size and criticality. They ship with the main consignment, clear customs with it, and sit on site from day one.
This is the right model for remote projects, for projects where the installer is not local, and for anything where a two-week wait for a part is unacceptable. The cost is visible in the quotation up front, which some buyers resist, but it is the cheapest way to guarantee a same-week repair.
Model two: factory stock, shipped on demand
No spares are purchased in advance. Parts are held at the plant and dispatched when a failure is confirmed. This suits distributors with a local warehouse, projects on a fast shipping lane, and buyers who would rather not tie up capital in stock that may never be used.
The trade-off is time. A part that has to be quoted, invoiced, packed and shipped internationally will not arrive this week. For a commercial system with a revenue loss per day, that arithmetic usually settles the question in favour of model one.
Pre-purchased spares ship with the main consignment and clear customs with it.
What spares cost
Spare parts are not free, including during the warranty period. The warranty covers the defective part; it does not cover a stock of replacements held on site. Pre-purchased spares are charged at the time of order and discounted against the project, with the discount depending on volume and mix.
Pre-purchased with the order
Shipped from factory stock
Quantity
Typically 3–5% of order
As required
Shipping
Travels with the main consignment
Separate shipment, separate customs
Cost timing
Paid with the order, discounted
Charged when the part is needed
Best for
Remote sites, non-local installers, high downtime cost
Local distributors, short shipping lanes, low downtime cost
Lead time after failure
Same day, part already on site
Quotation, then production and shipping
Repair after the warranty ends
Batteries, hybrid inverters and ESS cabinets carry a three-year warranty. Solar roof tiles carry a 25-year linear power warranty. Once those have expired, or where a fault is not covered, repair is charged at cost: no margin on the part, no fixed call-out fee.
There are two routes, priced differently.
Remote support. Diagnosis, configuration guidance and firmware work over email, messaging or video call. Provided without charge beyond the component cost, because it costs engineering time rather than travel.
Engineer on site. Used when the problem cannot be resolved remotely. The engineering time is not the expensive part. The travel, accommodation, visa and local transport are, and those are charged to the buyer at cost.
The practical advice is to exhaust the remote route first. Most faults that look like they need a site visit turn out to be configuration or communication problems that a scheduled call with the right photographs will resolve. Where attendance is genuinely required, the travel cost is quoted before anything is booked, so there is no invoice surprise afterwards. Requests start on the contact page, with the model and serial number in the first message.
Where this model fails
Being specific about the limits is more useful than another list of capabilities.
No 24/7 coverage. A fault on Friday evening is answered on the next business day. Acceptable for residential; for commercial systems with revenue at stake, it argues for pre-purchased spares and a local technician who can act on written instructions.
No regional service network. There is no partner in your country who can arrive the same day. If that is a project requirement, it has to be built locally, and it is better to know that at quotation stage.
Language limits on live calls. Written English is not a constraint; a spontaneous technical conversation in a second language is. Schedule calls and involve a translator where needed.
Support is not a substitute for a competent installer. Four of the five failures above are installation errors. The engineering team can diagnose and advise, but it cannot install a roof remotely, and the biggest determinant of how a project goes is who is on the roof.
For the installation side of that equation, see how the tile system is installed by one person. For the approval and sample stage that comes before a project order, see how sample customization works. For customization scope and certification by market, see the full-chain customization guide. For territory and stock terms, the distributor programme covers the commercial framework.
Frequently asked questions
How quickly does GreenMore respond to a technical question?
Typically within 24 hours on business days, and that means a substantive answer rather than an acknowledgement. Requests that arrive with a model number, serial number, fault code and photographs are usually resolved in the first reply. Missing serial numbers are the most common cause of a second round of questions.
What languages does technical support cover?
English is the working language. For other languages we work through a translator or machine translation, which is fine for documents and written questions but slow for a live fault-finding call. If the installation team does not work in English, nominate one English-speaking coordinator on the buyer side and schedule calls rather than improvising them.
Should I buy spare parts with the order?
If the site is remote, the installer is not local, or downtime has a real cost, yes. Pre-purchased spares are typically 3 to 5 percent of the order quantity, travel with the main consignment and are discounted against the project. If you hold a local warehouse or the project is on a fast shipping lane, factory stock shipped on demand is usually cheaper overall.
Are spare parts free during the warranty period?
No. The warranty covers the defective part, not a stock of replacements held on site. Pre-purchased spares are charged at the time of order and discounted against the project. Replacement of a covered failure is provided under the warranty terms, but spares held in reserve are not.
What happens after the warranty expires?
Repair is charged at cost, with no margin on the part and no fixed call-out fee. Remote diagnosis and configuration support are provided without charge beyond the component cost. If an engineer needs to attend site, travel, accommodation and local transport are charged to the buyer at cost, quoted before anything is booked.
Can I speak directly to an engineer?
Yes, for installation difficulties, commissioning problems and confirmed faults. Day-to-day questions normally go through your sales contact, who routes them to the right engineer and stays on the call as translator where needed. Direct engineer sessions are scheduled rather than immediate, so bring the drawing, the fault log and photographs.
S
Smith
Technical Director
Leads engineering support from system planning through long-term operation, reviewing designs and commissioning plans with partners before energizing.
Updated on November 14, 2026


 Network Supported